Developing and supplying quality pharmaceutical ingredients with a focus on consistent standards, reliable processes and long-term partnerships.
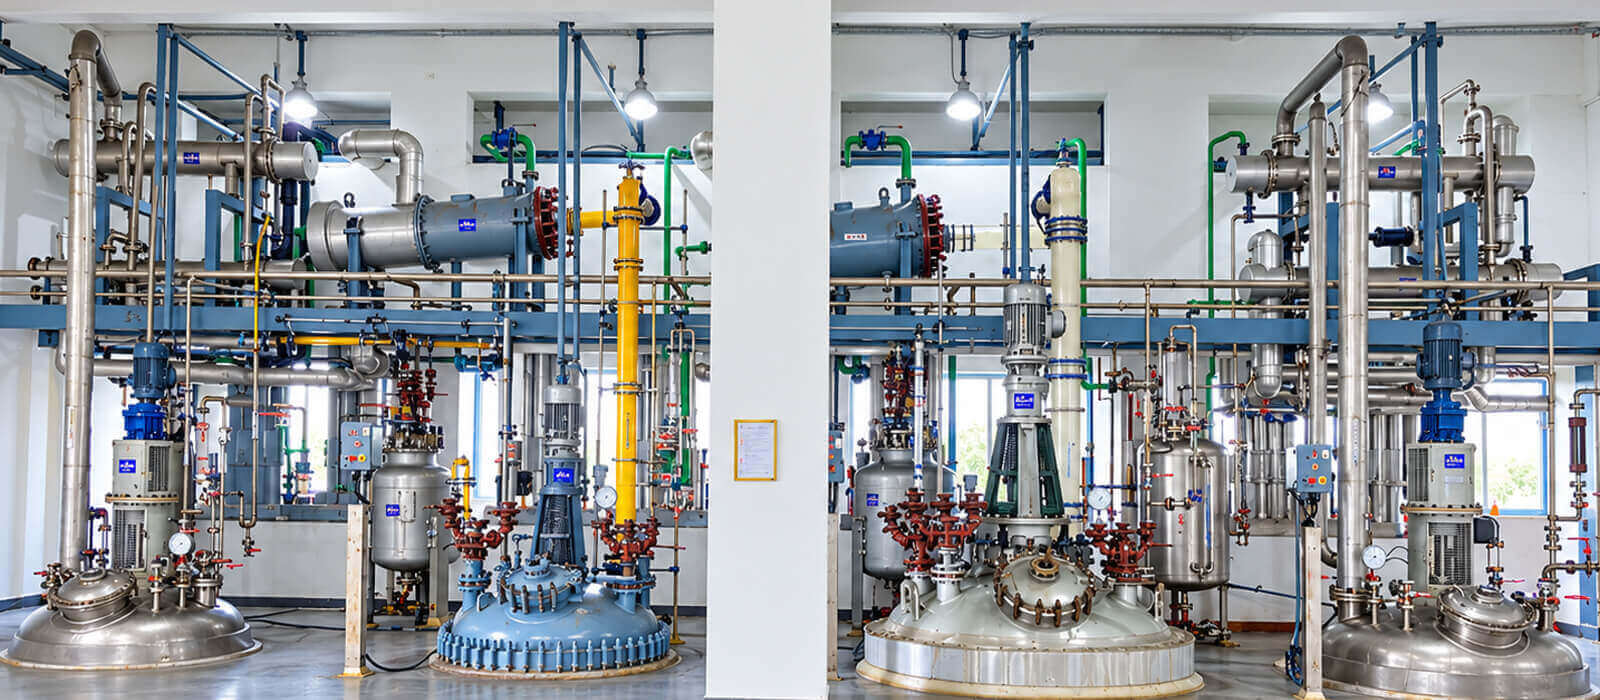
Pharmaceutical development to manufacturing, we follow controlled processes and quality practices to meet the changing needs of the industry.
We are leading manufactures of Oxetacaine, Mephentermine sulphate, Carbimazole, Methimazole, Nitazoxanide, Nitrofurantoin, Nitrofurazone, Rosuvastatin and Perindopril, with annual capacity of 150 MT. All products are manufactured using state of art technology with highest quality in WHO-GMP certified facility.
High-quality Active Pharmaceutical Ingredients, manufactured with a focus on purity, consistency and reliable supply.
Commercial API components are manufactured to meet diverse industrial and commercial requirements. With precise dimensions, consistent quality, and reliable performance, they are suitable for applications where durability and dependable functionality are essential.
View more
Livmore Life Sciences combines focused API manufacturing, quality systems and technical expertise to deliver consistent pharmaceutical ingredients for diverse market requirements.
Focused on the development and manufacturing of Active Pharmaceutical Ingredients with controlled processes and technical expertise.
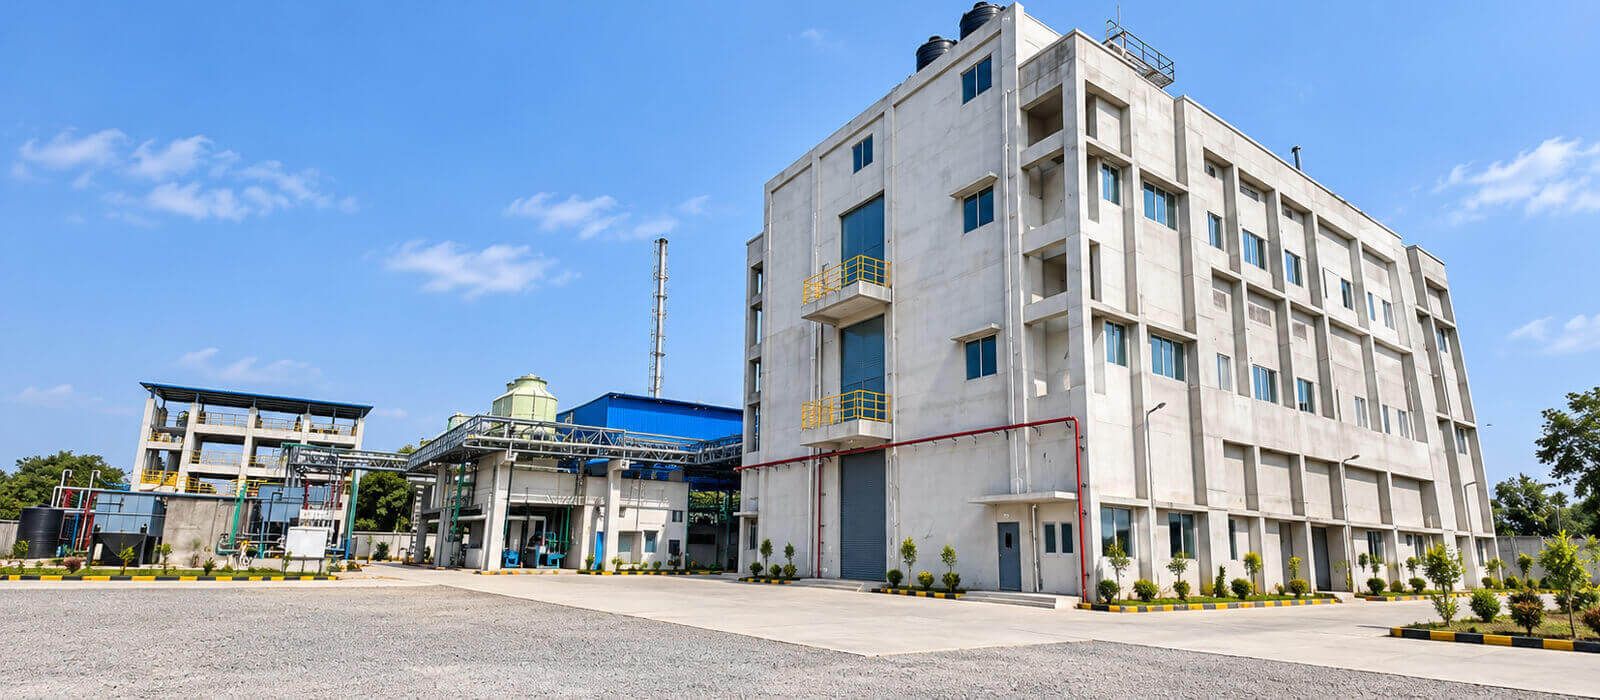
Well-equipped manufacturing facilities support controlled production, process consistency and dependable supply.
Quality is maintained through defined processes, testing and systematic controls across manufacturing activities.
Continuous process development and technical improvement support new products and evolving pharmaceutical requirements.
Since 2016, Livmore Life Sciences has been focused on the development and manufacturing of Active Pharmaceutical Ingredients, advanced intermediates and specialty chemicals.
Annual Manufacturing Capacity (MT)
Installed Reaction Capacity
Commercial API Products
Quality Commitment
Total Facility Area (Sq. M.)
Livmore Life Sciences supplies APIs and advanced intermediates to pharmaceutical markets, supporting customers with consistent quality, reliable manufacturing and responsive service.
View countriesEquipped with modern technology, precision manufacturing, and world-class qualitysystems to deliver trusted pharmaceutical solutions.
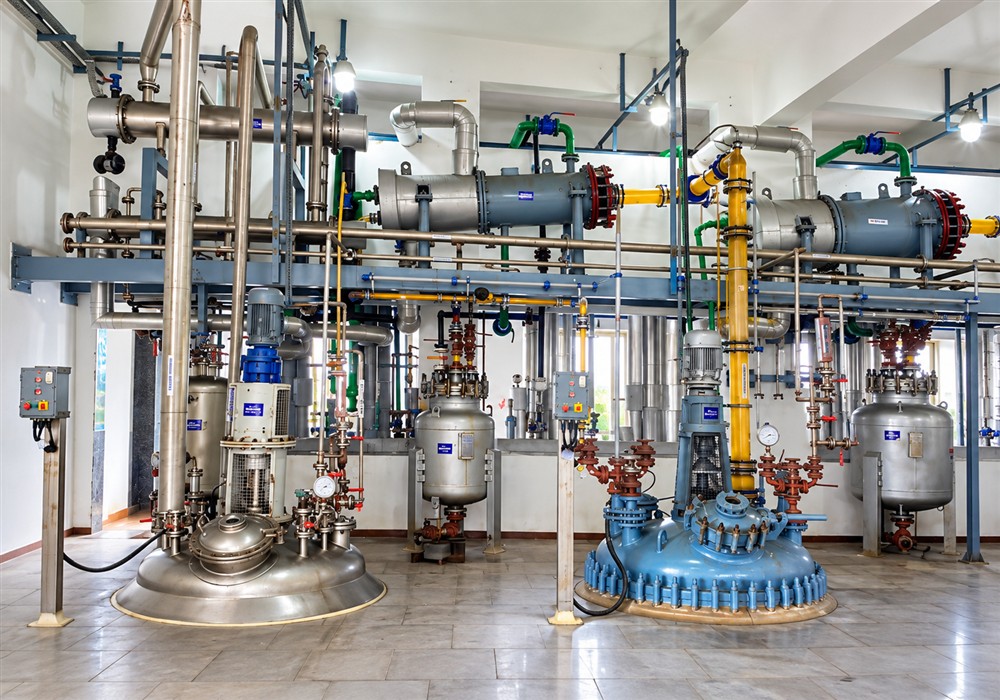
Controlled API manufacturing facilities with reactor systems, process areas and infrastructure for steady production needs.
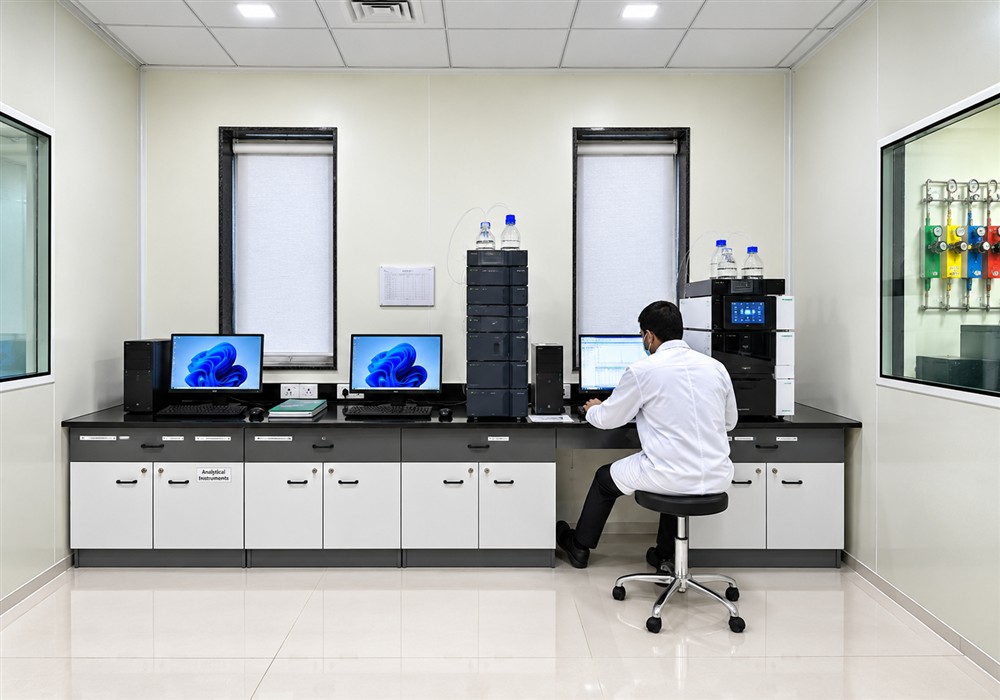
Dedicated R&D facilities support process development, product improvement and scale-up studies for pharmaceutical ingredients.
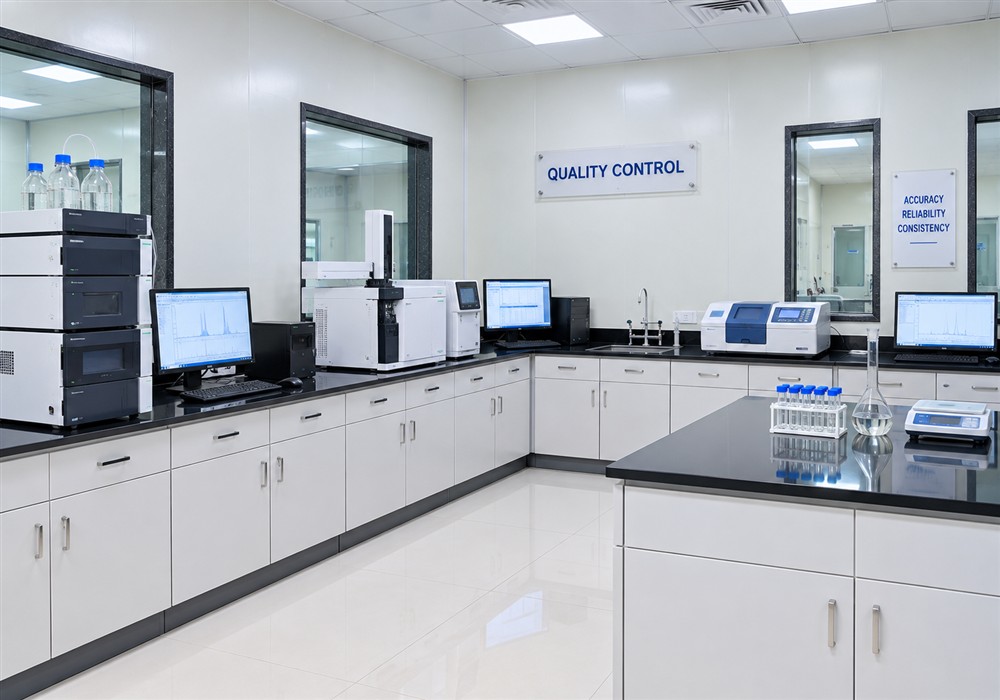
Quality control facilities support analytical testing of raw materials, in-process samples and finished API ingredients.
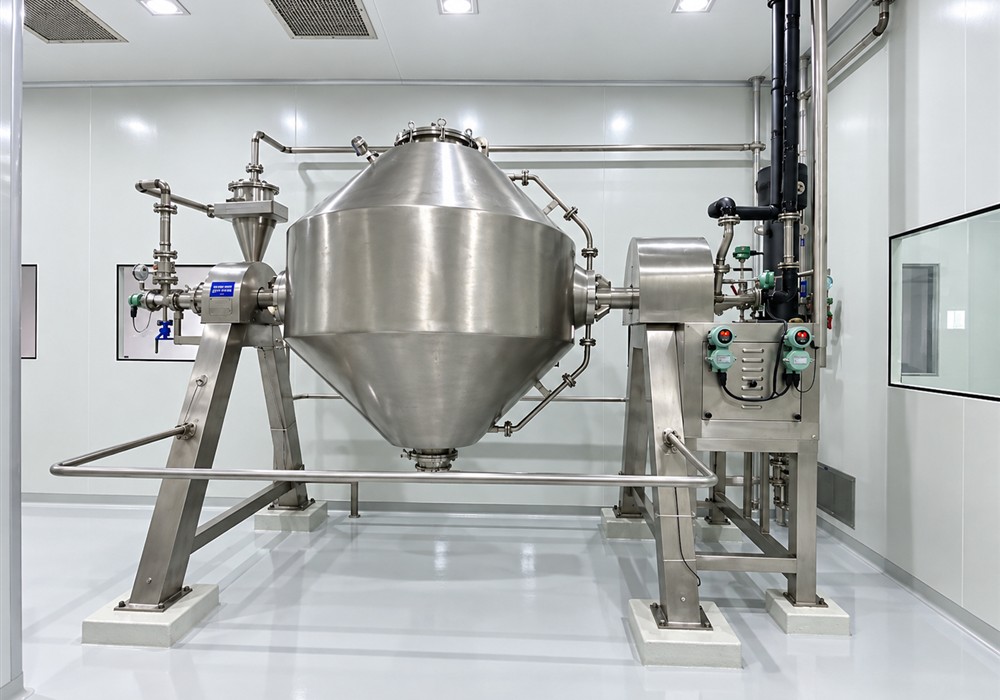
Process and drying equipment supports product handling, moisture removal and controlled steps during API manufacturing operations.
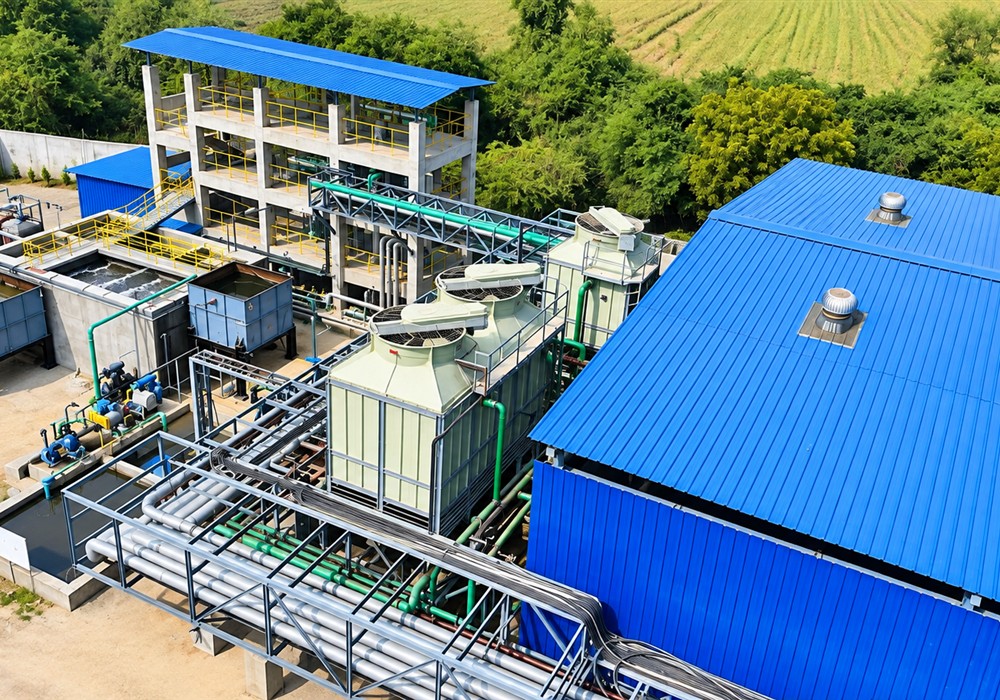
Effluent treatment facilities support handling and treatment of wastewater generated through plant manufacturing activities.
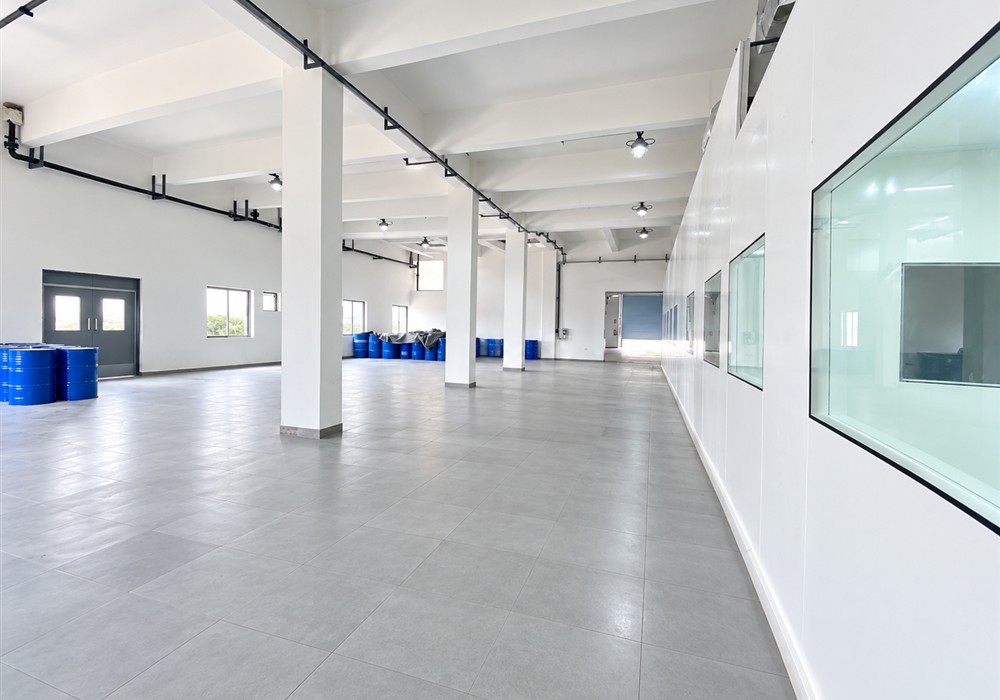
Warehouse and plant infrastructure provides space for material handling, storage, movement and daily supporting operations.
Every certificate we hold reflects how we think, work, and deliver. From quality to safety and sustainability, our processes are audited, approved, and alignedwith the highest global expectations.
Recognized by PMDA standards for quality, safety, and reliable pharmaceutical manufacturing.
Certified to ISO 9001, ISO 14001 and ISO 45001 standards for quality, environment, and safety.
Certified to SA 8000 standards supporting ethical practices, worker welfare, and responsibility.
Certified Kosher for compliance with recognized requirements for quality and product standards.
Certified Halal to meet accepted standards for quality, process control, and product purity.
We reduce our environmental impact through responsible resource use, efficient processes and proper waste management across our manufacturing operations.
We value our people and communities by promoting a safe workplace, responsible practices and positive relationships with employees and the wider community.
We follow defined systems, ethical practices and applicable industry requirements to maintain transparency, accountability and responsible business operations.
Survey No. 424, 431, Nana Fofaliya Road,
Vill. Ganpatpura, Karjan, Vadodara - 391210 (Guj.-Ind)